
A 4-inch pipe and a 4-inch flange share the same nominal size, but not always the same bore. Order a weld neck flange bored for schedule 40 and weld it to schedule 10S pipe, and the joint closes up with an internal step, a mismatched weld preparation and a root gap nobody planned for. Nothing in the part numbers looks wrong. The schedule was simply left out of the enquiry.
Nominal size tells you which pipe a flange belongs to. The schedule tells you how much steel that pipe carries, and therefore what the bore has to be. This guide covers that relationship for stainless flanges: how each flange type handles the bore, and what to put in an RFQ so the two arrive matched. It is general technical information; the governing standard edition, the project specification and a qualified engineer decide the final selection.
What nominal size fixes, and what the schedule changes
NPS is a designation, not a measurement. From NPS 1/8 upward the outside diameter is standardised and fixed; DN is the metric counterpart. Wall thickness is not fixed by size at all — it is set by the schedule. That split is the basis of matching flanges to pipe.
| Parameter | Changes with pipe schedule? | Defined by |
|---|---|---|
| Pipe outside diameter | No | NPS/DN dimension tables in ASME B36.10M and B36.19M |
| Pipe wall thickness and inside diameter | Yes | Schedule number |
| Flange outside diameter, bolt circle, thickness | No | Size and class, ASME B16.5 |
| Weld neck bore | Yes | Pipe schedule, ASME B16.5 bore tables |
| Slip-on bore | No — it clears the pipe outside diameter | Size and class |
| Flange pressure rating | No | Class, material group and temperature |
Two consequences follow. A flange of a given size and class fits the pipe of that size whatever schedule it carries, because the outside diameter never moves. And the schedule only becomes visible where the flange meets the pipe wall: at the bore and the weld preparation around it.
Reading the stainless schedule series
ASME B36.10M tabulates wrought steel pipe dimensions; ASME B36.19M does the same for stainless pipe and adds the lighter schedules used in corrosion-resistant lines: 5S, 10S, 40S and 80S. The S suffix identifies the schedule series tabulated in B36.19M. It does not stand for seamless — welded and seamless pipe of the same NPS and schedule share identical dimensions.
| NPS | Outside diameter (mm) | SCH 10S (mm) | SCH 40 (mm) | SCH 40S (mm) | SCH 80 (mm) | SCH 80S (mm) |
|---|---|---|---|---|---|---|
| 2 | 60.3 | 2.77 | 3.91 | 3.91 | 5.54 | 5.54 |
| 4 | 114.3 | 3.05 | 6.02 | 6.02 | 8.56 | 8.56 |
| 6 | 168.3 | 3.40 | 7.11 | 7.11 | 10.97 | 10.97 |
| 8 | 219.1 | 3.76 | 8.18 | 8.18 | 12.70 | 12.70 |
| 10 | 273.1 | 4.19 | 9.27 | 9.27 | 15.09 | 15.09 |
| 12 | 323.9 | 4.57 | 10.31 | 9.53 | 17.48 | 12.70 |
Up to NPS 10 the S schedules coincide with the plain ones; from NPS 12 they separate. A 12-inch line ordered as SCH 40S carries a 9.53 mm wall against 10.31 mm for SCH 40, about 1.6 mm of bore. On NPS 4 the gap is larger — 3.05 mm against 6.02 mm, which moves the inside diameter from about 108.2 mm to about 102.3 mm. Small on a drawing, impossible to ignore at the weld.
How each flange type handles the bore
Weld neck: the bore follows the schedule
A weld neck flange is butt welded to the pipe, so the bore has to line up with the pipe inside diameter and the bevel with the pipe wall. ASME B16.5 tabulates the bore as dimension B by pipe schedule, which means the schedule is part of the identity of the part. A weld neck ordered without a schedule cannot be finished to the correct bore, and a flange bored to the wrong schedule cannot be corrected by welding technique.

Slip-on: the bore clears the outside diameter
A slip-on flange slides over the pipe and is fillet welded at both ends. Its bore is fixed by size and class and is deliberately larger than the pipe outside diameter. Because the outside diameter is the same for every schedule, one slip-on boring serves all schedules of that size — the schedule does not change the flange, but it does change the weld, since a thin wall offers less throat for the fillet.
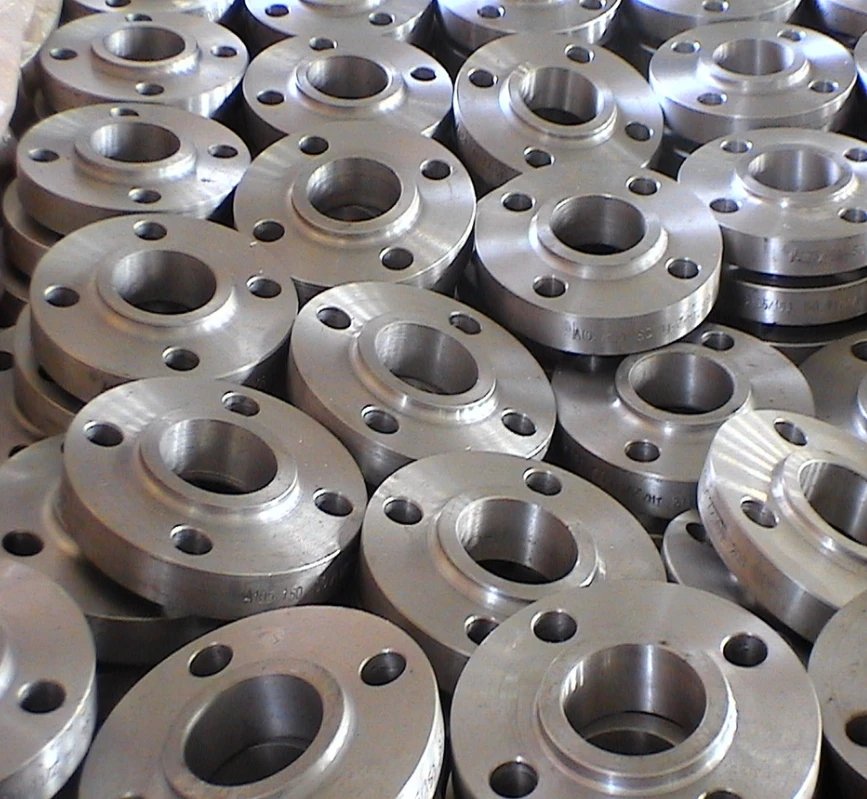
Plate and blind: only one of them has a bore
A blind flange has no bore, so schedule is irrelevant to the part. A plate flange bored for welding is a different case: the bore is machined to take the pipe, normally with clearance for assembly, and the schedule governs the wall that will be welded to it rather than the flange dimensions.
| Flange type | Bore rule | Schedule needed in the RFQ? | Attachment |
|---|---|---|---|
| Weld neck | Machined to the pipe inside diameter for that schedule | Yes — the bore cannot be defined without it | Butt weld |
| Slip-on | Fixed clearance over the pipe outside diameter | Not for the boring; state it for weld procedure and NDE | Two fillet welds |
| Plate | Bored with clearance to the pipe outside diameter | Yes, for the weld and the bore size | Fillet or butt weld, per design |
| Blind | None | No | None — bolted only |
What a bore mismatch looks like on site
Two failures account for most problems; both are visible before anyone strikes an arc.
- Bore too small. A weld neck bored for a heavier schedule than the pipe presents a bore smaller than the pipe inside diameter. The result is an internal ledge at the joint, a wall step at the bevel and a root gap that has to be closed by deposition rather than fit-up. On lines that are pigged or cleaned in place, the ledge is also a trap.
- Bore too large. A weld neck bored for a lighter schedule leaves the bore wider than the pipe inside diameter. The bevel no longer meets a matched wall, root fusion is difficult to control, and the internal step faces the other way.
Neither is covered by the standard’s intent: B16.5 bores are tabulated so that a weld neck and a pipe of the same size and schedule produce a matched-wall butt joint. Mismatched schedules make the joint a fabrication decision, and it belongs with the piping engineer before welding.
Where schedule 10S lines cause the most trouble
Thin-wall stainless is common in food, pharmaceutical, water treatment and low-pressure chemical service, and it is exactly where bore mismatches appear. A buyer accustomed to carbon steel quotes “4-inch, class 150, weld neck” and receives a flange bored to SCH 40 while the pipe on site is SCH 10S: correct to its own order, wrong for the line. The reverse happens when a stock flange bored for SCH 10S is issued against a heavier SCH 40 line. One line in the enquiry prevents both.
What to write in the RFQ
Most schedule problems are created at the enquiry stage, and a short checklist removes them:
- Standard and edition: ASME B16.5, with the edition the project is designed to.
- Size and schedule together: NPS 4 SCH 10S, not “4 inch”.
- Flange type and facing: weld neck, slip-on, plate or blind, with RF, FF or RTJ.
- Bore instruction: “bored to match SCH 10S”, or the inside diameter when the pipe is not to a standard schedule.
- Flush bore requirement: state it where the line is pigged, hygienic or internally inspected, so no step is accepted.
- Material and certificate: ASTM A182 grade such as F304L or F316L, with the certificate type — 3.1 is the usual baseline for pressure-retaining forgings.
- Weld preparation: whether the bevel is supplied on the flange or prepared by the fabricator.
- Marking and packing: heat traceability and protection of the machined bore and sealing face.
The schedule is the one item that cannot be inferred from a flange drawing.
Frequently asked questions
Does the S in SCH 10S mean seamless?
No. The S identifies the schedule series tabulated in ASME B36.19M for stainless steel pipe. Both seamless and welded pipe can be supplied as SCH 10S, and their dimensions are identical for the same size and schedule.
Will a slip-on flange bored for SCH 40 fit a SCH 10S pipe?
Yes — the bore clears the pipe outside diameter, the same for both schedules, so the pipe passes through. The difference appears at the weld: thin-wall pipe offers less thickness for the fillet, so the weld procedure should be confirmed for that wall rather than assumed from the flange order.
Can a SCH 40 weld neck flange be used on SCH 10S pipe?
Not as a matched-wall joint. A weld neck bored for SCH 40 has a bore smaller than the SCH 10S pipe inside diameter, so the joint closes with an internal step and a wall mismatch at the bevel. The correct order is a weld neck flange bored for the actual schedule of the pipe.
Does the schedule change the flange pressure rating?
No. The rating comes from class, material group and design temperature, read from the ASME B16.5 tables. Schedule affects the pipe wall and, for a weld neck, the bore — it does not raise or lower the rating.
Is NPS the same as the pipe outside diameter in inches?
Only from NPS 14 upward. Below that it does not: NPS 4 pipe has a 114.3 mm outside diameter, not 101.6 mm. NPS is a designation used to look up dimensions, not a measurement.
Conclusion
The dimensional chain is short and unforgiving. NPS fixes the outside diameter, the schedule fixes the wall, and the bore has to follow the wall wherever a butt weld joins flange to pipe. Weld neck flanges therefore carry the schedule in their specification; slip-on and blind flanges do not.
Write the schedule next to the size in every enquiry, state whether a flush bore is required, and confirm the final selection against the applicable standard, the project specification and a qualified engineer before fabrication.
Need stainless flanges bored to your pipe schedule, with matching documentation? Send the size, schedule, class, facing and grade through our contact page and our team will confirm what can be supplied and certified. You can also review the weld neck flange range, the slip-on flange range where a clearance bore is acceptable, or a 2-inch SCH 40S weld neck flange to ASME B16.5 as a reference for how the schedule is written into a part description.
References
ASME. B36.10-2022 – Welded and Seamless Wrought Steel Pipe.
ASME. B36.19-2022 – Welded and Seamless Wrought Stainless Steel Pipe.
ASME. B16.5-2020 – Pipe Flanges and Flanged Fittings: NPS 1/2 through NPS 24, Metric/Inch Standard.